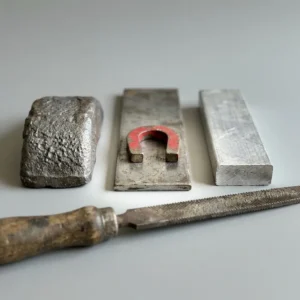
Metal identification chart in short: a magnet sticks hard to both mild steel and cast iron, but on a grinder mild steel throws a spark stream about 70 in (178 cm) long and gray cast iron a dull red one of about 25 in (64 cm). Work through four shop tests below in order (magnet, look and weight, file or chisel, spark) and pick what you see. You get the most likely metal, from mild and high-carbon steel to cast iron, stainless, aluminum, brass and pot metal, and how to weld it. Shop tests narrow a metal down; they do not prove an alloy.
Compiled by Welding Tribe from the published sources listed below. Answers last updated on .
Identify a metal in four tests
Work through the tests in order: a magnet, a look at the color and weight, a file or chisel, then a grinder. Pick what you see at each step to get the most likely metal and how to weld it. Leave a test at “Not tested” until you have run it.
Mild steel
Low-carbon steel, 0.30% carbon or less, is the best match.
- How sureGood matchEvery test you ran fits.
- Could also beMedium-carbon steelMore bursts in the sparks.
- Caution
- How to weld itAny common processThick sections: low-hydrogen rod such as E7018.Stick welding amperage chart
- These tests narrow it down; they don’t prove an alloy. Spark test: safety glasses, face shield, no fuel nearby.
Show the working
- Magnet sticks hard: iron, carbon steel, or a ferritic, martensitic or duplex stainless, which a magnet grips strongly (ASSDA).
- Gray, heavy and rusting: iron or carbon steel. Rolled steel shows fine lines in one direction; forgings show hammer marks or a fin (Army TM 9-237).
- File bites and chips curl: a tough metal that does not break short, as steel and cast steel are (Army TM 9-237).
- Long sparks with a few forked bursts: low-carbon steel, about 70 in (178 cm) on the Navy’s bench wheel. The Navy calls the stream white; the Army calls it yellow-orange, bursting into white forks.
- Welding: low-carbon steel is readily welded by all methods (Army TC 9-524). TWI adds that thick sections need hydrogen control, such as a low-hydrogen rod, or preheat.
- Limits: these tests sort metal into families. They can’t name an alloy or a heat treatment. For lifting gear, trailer and vehicle parts and anything under pressure, get a lab test or the material certificate.
Metal identification chart
What each common shop metal does in the four tests, and how to weld it. The chart is compiled from the US Army’s and Navy’s welding and metalworking manuals, with the stainless magnet facts from the Australian Stainless Steel Development Association and the welding notes from TWI. A dash means our sources say nothing for that test.
| Metal | Magnet | Look and weight | File or chisel | Spark | How to weld it |
|---|---|---|---|---|---|
| Mild (low-carbon) steel | Sticks hard | Gray; rusts. Fine rolling lines, or forging marks | File bites; chips curl and are tough | About 70 in (178 cm). White to yellow-orange, a few forked bursts | Any common process. Thick sections: low-hydrogen rod such as E7018. Stick welding amperage chart |
| Medium- and high-carbon steel | Sticks hard | Dark gray; rusts. Springs, tools, blades | File bites when soft, skates when hardened | About 55 in (140 cm). More volume, many small repeating bursts | Preheat, low-hydrogen rod. It hardens and cracks beside the weld. Don’t weld springs. Welding rod chart |
| Wrought iron | Sticks hard | Like rolled mild steel; a break looks fibrous | — | About 65 in (165 cm). Straw near the wheel, a few forks near the end | Gas or arc weld. The Army manual lists it as weldable both ways. Stick welding amperage chart |
| Gray cast iron | Sticks hard | Very dull gray, rough sand-cast skin; dark gray break | Chips break off as they form | About 25 in (64 cm). Small volume, dull red, straw at the end | Nickel or nickel-iron rod. Preheat near 570°F (300°C), short beads, peen, cool slowly. Stick welding amperage chart |
| Malleable iron | Sticks hard | Dull gray casting, mostly free of sand; a break shows a bright rim round a dark center | Tough; doesn’t break short | Bright like steel at the skin, then dull red; longer and fuller than gray iron | Nickel or nickel-iron rod. Low heat and slow cooling. Preheat depends on the type. Stick welding amperage chart |
| White (chilled) cast iron | Sticks hard | Casting; silvery white break | File skates: very hard and brittle | — | Don’t weld it. TWI rates white cast iron as normally unweldable. |
| Cast steel | Sticks hard | Casting, brighter than cast iron; may show small bubble-like pits | Tough; chips curl | Much brighter than cast iron | Weld as carbon steel. Over 0.5% carbon it gets difficult: preheat, low-hydrogen rod. Welding rod chart |
| Stainless, 300 series (304, 316) | Doesn’t stick, or weakly after cold work | Silver; no rust | — | About 50 in (127 cm). Straw near the wheel, white at the end, a few forks | 308L filler for 304. 309L to join it to mild steel. 316 takes its own filler. Stainless steel welding rod chart |
| Stainless, 400 series (409, 410, 430) | Sticks hard | Silver; no rust | — | Straw, then white (given for stainless as a whole) | Filler by grade. 409, 410 and 430 differ, and 410 needs preheat. Stainless steel welding rod chart |
| Nickel and Monel | — | Grayish white; Monel looks like stainless | — | A few short, wavy orange streaks; no bursts | Gas or arc weldable (Army TC 9-524). Have the alloy confirmed before you pick a filler. |
| Aluminum | Doesn’t stick | Light gray to silver; about a third the weight of steel | — | No sparks | TIG or MIG, 4043 or 5356. Brush the oxide off first. The alloy decides the filler. Aluminum filler rod chart |
| Magnesium | Doesn’t stick | Silver-white, turns gray; about two-thirds the weight of aluminum | — | No sparks, but don’t grind it: the chips burn | Leave it to a specialist shop. Its chips are highly flammable and its fires can’t be put out with ordinary extinguishers (Army TC 9-524). |
| Copper, brass and bronze | Doesn’t stick | Copper is reddish brown and weathers green; brass and bronze run yellower | — | No sparks | Braze or solder. The Navy also lists gas and arc welding. Brass fume carries zinc. Oxy-acetylene torch settings chart |
| Zinc die cast (pot metal) | Doesn’t stick | Blue-white when polished, gray when weathered; grainy break | — | No sparks | Low-heat repair only. Zinc melts near 787°F (419.5°C). Don’t weld or grind lead. Can you weld pot metal? |
| Lead | Doesn’t stick | Gray-white, soft and very heavy | — | No sparks | Don’t weld or grind it: its dust, fumes and vapors are highly poisonous (Navy Steelworker course). |
Shop tests narrow a metal down to a family. They do not prove an alloy, a carbon content or a heat treatment, and a wrong guess can crack a repair. For lifting gear, trailer and vehicle parts and anything under pressure, get a lab test or the material certificate before you weld.
Once you know the metal, the stick welding amperage chart and the welding rod chart cover mild steel rods, the stainless steel welding rod chart picks a stainless filler, and the TIG welding settings chart has aluminum and stainless settings.
Spark test chart for metals
The spark stream each metal throws, from the US Navy’s Steelworker course. Its lengths are for a coarse, hard, clean bench wheel with a rim speed of at least 4,500 ft/min. The Army’s machine tool manual uses a portable grinder instead, with just enough pressure for a stream about 12 in (30 cm) long. So read the lengths as a ranking, not a ruler, and grind a piece of known steel the same way to compare. The two services also describe the colors differently: both are shown.
| Metal | Stream length | Volume | Color | Bursts |
|---|---|---|---|---|
| Low-carbon (mild) steel | About 70 in (178 cm) | Moderately large | White (Navy); yellow-orange, bursting white (Army) | Few, forked |
| High-carbon steel | About 55 in (140 cm) | Larger than mild steel | White (Navy); brilliant yellow-orange (Army) | Many, small and repeating |
| Wrought iron | About 65 in (165 cm) | Large | Straw near the wheel | Few, forked, near the end |
| Gray cast iron | About 25 in (64 cm) | Rather small | Red near the wheel, straw at the end | Small and repeating |
| Stainless steel | About 50 in (127 cm) | Moderate | Straw near the wheel, white at the end | Few, forked |
| Nickel and Monel | Short (no figure given) | Small | Orange, wavy streaks | None |
| Aluminum, magnesium, copper, zinc, lead | No sparks | — | — | — |
Weight for its size
Heft the part against a piece of steel about the same size. Aluminum and magnesium feel far too light, lead far too heavy; zinc, cast iron, stainless and brass are too close to steel to sort by hand. Densities are from Engineering ToolBox.
| Metal | Weight | Times the weight of steel |
|---|---|---|
| Magnesium | 108 lb/ft³ (1,738 kg/m³) | 0.22 |
| Aluminum | 169 lb/ft³ (2,712 kg/m³) | 0.35 |
| Zinc | 445 lb/ft³ (7,135 kg/m³) | 0.91 |
| Cast iron | 425–487 lb/ft³ (6,800–7,800 kg/m³) | 0.87–0.99 |
| Steel | 490 lb/ft³ (7,850 kg/m³) | 1.00 |
| Stainless steel | 467–499 lb/ft³ (7,480–8,000 kg/m³) | 0.95–1.02 |
| Yellow brass | 529 lb/ft³ (8,470 kg/m³) | 1.08 |
| Copper | 558 lb/ft³ (8,940 kg/m³) | 1.14 |
| Lead | 708 lb/ft³ (11,340 kg/m³) | 1.44 |
How to run the four tests
- Magnet. Put a small magnet on a clean, bare spot and note a hard pull, a weak pull or none. It splits iron and steel from the rest, but not perfectly: some stainless steel is non-magnetic.
- Look and weight. File or scrape a spot down to bare metal and note its color. Look for rust, a rough sand-cast skin, fine rolling lines or forging marks, then heft the part against steel of the same size.
- File or chisel. Draw a sharp file across an edge: it bites into soft metal and skates over metal harder than itself. Then lift a small chip with a cold chisel and see whether it curls or breaks off. Wear safety glasses: chips fly.
- Spark test, last. Wear safety glasses with side shields under a face shield, and keep sparks away from fuel, rags and gas cylinders. Touch the metal lightly to a clean wheel: heavy pressure makes the carbon look higher than it is. Never grind light, silver-white metal that could be magnesium, soft gray metal that could be lead, or plated and painted parts without ventilation.
Quick answers
How can I tell cast iron from cast steel?
With a chisel and a grinder; a magnet sticks hard to both. Gray cast iron chips break off as they form, and its sparks are short, thin and dull red, about 25 in (64 cm). Cast steel is tough: its chips curl, and its sparks are much brighter, like other steel. If the two tests disagree, don’t weld it until you are sure.
How do I tell if metal is cast iron?
Gray cast iron has a very dull gray, rough sand-cast skin and a dark gray break. A magnet sticks hard, a chisel lifts chips that break off instead of curling, and a grinder throws a small, dull red spark stream about 25 in (64 cm) long, against about 70 in (178 cm) for mild steel.
What does a spark test tell you?
Roughly how much carbon is in iron or steel. Mild steel throws a stream about 70 in (178 cm) long with a few forked bursts, high-carbon steel about 55 in (140 cm) with many small repeating bursts, and gray cast iron a dull red one about 25 in (64 cm) long. It cannot name an alloy, so compare against a piece of known steel.
Is stainless steel magnetic?
Some of it. The stainless association ASSDA says 304 and 316 are non-magnetic when annealed but can pick up some pull from cold work, and that ferritic grades such as 409, martensitic grades and duplex grades hold a magnet strongly. So a magnet that sticks does not rule stainless out, and one that falls off does not prove it.
Is it aluminum or stainless steel?
Heft it first. Aluminum weighs about 169 lb/ft³ (2,712 kg/m³) and stainless steel 467–499 lb/ft³ (7,480–8,000 kg/m³), close to three times as much. If it is that light you have your answer, and there is no need to grind it. Stainless throws a spark stream about 50 in (127 cm) long; aluminum throws none.
How can I tell mild steel from high-carbon steel?
By the sparks and a file. Mild steel throws a stream about 70 in (178 cm) long with a few forked bursts. High-carbon steel throws a fuller one, about 55 in (140 cm), with many small repeating bursts, and a file skates over it once it is hardened. Springs, tools and blades are the usual high-carbon parts.
Is it aluminum or magnesium?
Go by weight, not by sparks: neither one sparks, and magnesium chips burn. Magnesium weighs about 108 lb/ft³ (1,738 kg/m³) against 169 lb/ft³ (2,712 kg/m³) for aluminum, about two-thirds as much. The Army manual’s test is a drop of silver nitrate solution, which leaves a black deposit on magnesium. If it could be magnesium, don’t grind or weld it.
Can you weld cast iron?
Gray and malleable cast iron, yes, with care. From the chart: Nickel or nickel-iron rod. Preheat near 570°F (300°C), short beads, peen, cool slowly. TWI adds that white cast iron is normally unweldable, and that braze welding is often used on castings to avoid cracking.
How do I know if it’s pot metal?
Pot metal (zinc die cast) does not hold a magnet, does not rust and gives no sparks. It is blue-white when polished and gray when weathered, with a grainy break, and it melts at a low temperature. From the chart: Low-heat repair only. Zinc melts near 787°F (419.5°C). Don’t weld or grind lead. See our guide to welding pot metal.
How accurate are magnet, spark and file tests?
Good enough to sort metal into families, not to prove an alloy. The Navy course says the magnet test is not 100% accurate because some stainless steels are non-magnetic, the Army manual says the spark test is not a positive one for vanadium steels, and a file only shows softer or harder than the file. For parts where a failure could hurt someone, get a lab test.
Two more cautions. Copper-colored springs, bushings and bearings can be copper-beryllium, and OSHA links breathing beryllium dust or fume to chronic lung disease and lung cancer: don’t grind or weld them. And clean plating, galvanizing and paint off before you weld, with ventilation: OSHA names zinc, cadmium and lead among the metals in harmful welding fume.
- Appearance, break, chip and spark notes for each metal, and what welds: US Army TM 9-237, “Welding Theory and Application” (1967 edition, checked against the 1976 edition). Stated in our own words.
- Spark stream lengths, volumes and bursts, the wheel speed and the limits of the magnet test: the US Navy Steelworker training course, “Metal identification”.
- The file test, carbon ranges and what they mean for welding, magnesium’s weight and fire risk, brass’s zinc content: US Army TC 9-524, “Fundamentals of Machine Tools”, chapter 2.
- Which stainless steels hold a magnet: ASSDA Technical FAQ 3. Welding cast iron, aluminum and carbon steel: TWI Job Knowledge 25, 21 and 19. Weights: Engineering ToolBox. Eye and face protection and welding fume: OSHA.
- Which metal the four answers point to, and “how sure”, is our own sorting of those published facts. It is a shop guide, not a laboratory method.
Answers compiled from the sources below and last updated on . Spotted a mistake? Tell us.
- US Army, TM 9-237, “Welding Theory and Application” (1967), chapter 2: appearance, fracture, spark and torch notes for each metal (public domain; Internet Archive)
- US Army, TM 9-237, “Operator’s Manual: Welding Theory and Application” (1976), chapter 2, as a cross-check (Internet Archive)
- US Army, TC 9-524, “Fundamentals of Machine Tools”, chapter 2: file test, spark test, carbon ranges, magnesium, brass
- US Navy, Steelworker training course, “Metal identification”: spark stream lengths, magnet test, surface appearance
- Australian Stainless Steel Development Association, Technical FAQ 3, “Magnetic Effects of Stainless Steels”
- TWI, Job Knowledge 25, “Weldability of materials: cast irons” (rods, preheat, technique)
- TWI, Job Knowledge 21, “Weldability of materials: aluminium alloys” (fillers, cleaning, alloys not to fusion weld)
- TWI, Job Knowledge 19, “Weldability of materials: carbon manganese and low alloy steels” (carbon, hardening, low-hydrogen practice)
- Engineering ToolBox, “Metals and Alloys: Densities”
- OSHA, 29 CFR 1910.133, eye and face protection (flying particles, side protection)
- OSHA Fact Sheet FS-3647, “Controlling Hazardous Fume and Gases during Welding” (coatings, zinc, cadmium, lead)
- OSHA, “Beryllium” (copper-beryllium parts and health effects)
- Zinc’s melting point is from Randy Williams’s guide “Can You Weld Pot Metal?”
Related welding guides
- Can you weld pot metal?
- Can you weld leaf springs?
- Why welding rods stick, and the amperage chart for mild steel rods
More free welding charts
- Stick Welding Amperage Chart by Rod Size
- Welding Polarity Chart: DCEP, DCEN or AC
- Stick Welding Amperage by Metal Thickness
- Beginner Welding Rod Chart and Rod Number Decoder
- Welding Rod Oven Temperature Chart
- Welding Shade Chart: Lens Shade by Process and Amps
- Welding Troubleshooting
- Welding Practice Test with Answers
- MIG Welding Settings Chart
- Welding Cable Size Chart
- Welding Gas Cylinder Calculator: How Long a Tank Lasts
- Welding Cost Calculator
- Welder Breaker Size Chart: Breaker, Wire and Outlet
- What Size Generator to Run a Welder? Calculator
- Oxy-Acetylene Torch Settings Chart
- Stainless Steel Welding Rod Chart: 308L, 309L, 316L
- TIG Welding Settings Chart
- Plasma Cutter Amps Chart: Amps and Air by Thickness
- Welder Duty Cycle Calculator: Weld Time at Any Amps
- Aluminum Filler Rod Chart: 4043 vs 5356 by Alloy
- What Size Welder Do I Need? Amps by Metal Thickness