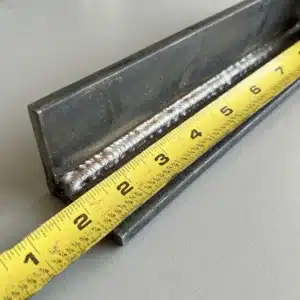
A 1/4 in fillet weld holds about 0.106 lb of steel per foot, so 10 ft of it with 1/8 in E7018 takes about 1.75 lb of rods and 1.6 hours of your time, allowing 10% for a convex face. Enter your own weld and prices in the welding cost calculator below for the filler, gas, time and a job price, from TWI’s cost method and ESAB and Lincoln data.
Price a welding job
Describe the weld and enter your own prices. You get the rods or wire to buy, the gas, the arc time and your time on the job, and a price. The prices filled in are examples only.
$83.29
Job price for 10 ft of 1/4 in fillet weld, 1/8 in E7018 rods, with 20% added
- Weld metal1.17 lb (0.117 lb per ft)
- To buy1.75 lb of rods (weld metal × 1.5)
- Arc time23 min at 3.0 lb per hour
- Your time1.6 h with the arc on 25% of the time, plus 0 min set-up
- Shielding gasNone
- Rods or wire
- $7.02
- Gas
- $0.00
- Your time
- $62.39
- Cost
- $69.41
- Per foot
- $8.33
Weld metal and filler per foot of fillet weld
Weld metal in a flat-faced, equal-leg fillet weld in steel (leg² ÷ 2 × length × 0.2836 lb per cubic inch), and how much to buy with TWI’s allowances for stubs, spatter and handling. Add a little for a convex face.
| Fillet leg | Weld metal, lb per ft | Weld metal, kg per m | Stick rods to buy, lb per ft | MIG wire, lb per ft | Flux core wire, lb per ft |
|---|---|---|---|---|---|
| 1/8 in | 0.027 | 0.040 | 0.040 | 0.028 | 0.032 |
| 3/16 in | 0.060 | 0.089 | 0.090 | 0.063 | 0.072 |
| 1/4 in | 0.106 | 0.158 | 0.160 | 0.112 | 0.128 |
| 5/16 in | 0.166 | 0.247 | 0.249 | 0.174 | 0.199 |
| 3/8 in | 0.239 | 0.356 | 0.359 | 0.251 | 0.287 |
| 1/2 in | 0.425 | 0.633 | 0.638 | 0.447 | 0.510 |
How long it takes to weld a foot of 1/4 in fillet
| Process and consumable | Deposition, lb per hour | Arc time per ft | Welder time per ft |
|---|---|---|---|
| Stick, 3/32 in E7018 | 2.0 | 3.2 min | 12.8 min (arc on 25%) |
| Stick, 1/8 in E7018 | 3.0 | 2.1 min | 8.5 min (arc on 25%) |
| Stick, 5/32 in E7018 | 4.2 | 1.5 min | 6.1 min (arc on 25%) |
| MIG, 0.030 in wire at 250 in/min | 2.9 | 2.2 min | 6.4 min (arc on 35%) |
| MIG, 0.035 in wire at 250 in/min | 3.9 | 1.6 min | 4.7 min (arc on 35%) |
| MIG, 0.045 in wire at 200 in/min | 5.2 | 1.2 min | 3.5 min (arc on 35%) |
| Gasless flux core, 0.035 in at 150 in/min | 1.7 | 3.8 min | 10.7 min (arc on 35%) |
| Gasless flux core, 0.045 in at 110 in/min | 2.3 | 2.8 min | 7.9 min (arc on 35%) |
Quick answers
How much weld metal is in a 1/4 inch fillet weld?
About 0.106 lb per foot (0.16 kg per meter) for a flat-faced, equal-leg fillet in steel: the cross-section is leg² ÷ 2 = 0.031 square inches. A convex face adds a little more.
How many pounds of 7018 rod do I need?
About 1.5 times the weld metal, to cover stub ends and losses: 0.16 lb of rods per foot of 1/4 in fillet, or about 1.6 lb for 10 ft. Allow more for a convex weld.
How much MIG wire do I need per foot of weld?
About 1.05 times the weld metal: 0.11 lb per foot of 1/4 in fillet. Flux core wire needs about 1.2 times, or 0.13 lb per foot.
How long does it take to weld a foot of fillet?
For a 1/4 in fillet, MIG with 0.035 in wire at 250 in/min takes about 1.6 minutes of arc time, or about 4.7 minutes of your time with the arc on 35% of the time. Stick with 1/8 in 7018 takes about 2.1 minutes of arc time, about 8.5 minutes in all at 25% arc-on.
How do I price a welding job?
Add up the filler, the gas and your time, then add overhead and profit. Your time is the arc time divided by the share of time the arc is actually on, plus set-up and fit-up. Labor is usually the biggest part.
How much of the time is the arc actually on?
Less than you think. TWI gives 15–30% for stick, 30–45% for MIG, 25–45% for flux core and 25–40% for TIG, before counting set-up and fit-up.
How fast does a 1/8 inch 7018 rod deposit?
ESAB measures about 3.0 lb per hour for a 1/8 in Atom Arc 7018 near the top of its current range, 2.0 lb for 3/32 in and 4.2 lb for 5/32 in. Each rod burns for roughly a minute.
How fast does MIG wire deposit?
It depends on the wire size and speed. 0.035 in wire at 250 in/min melts about 4.1 lb per hour and deposits about 3.9 lb per hour; 0.045 in at 200 in/min deposits about 5.2 lb per hour.
- Filler factors (stick 1.5, MIG 1.05, flux core 1.2) and arc-on time by process: TWI, Job Knowledge 96, “Welding costs”. Deposition rates and method: TWI, Job Knowledge 97.
- Stick deposition: ESAB, Atom Arc 7018 deposition data, at 90% of each size’s top current, with burn-off times of 60–75 seconds per 14 in rod.
- Wire: melt-off from wire size, speed and steel’s density, checked against Lincoln Electric’s SuperArc L-56 data sheet; gasless deposition from Lincoln’s Innershield NR-211-MP data sheet.
- Weld metal: fillet cross-section leg² ÷ 2, steel at 0.2836 lb per cubic inch (7.85 g/cm³). Prices are yours to enter; the ones filled in are examples, not market prices.
- Labor as the biggest cost: Miller Electric puts labor at about 85% of the cost of making a weld (“How to Choose MIG Welding Consumables to Optimize Productivity”).
Numbers checked on by Randy Williams against the sources below. Spotted a mistake? Tell us.
- TWI, Job Knowledge 96, “Welding costs” (filler factors, arc-on time)
- TWI, Job Knowledge 97, “Welding costs – continued” (deposition rates)
- ESAB, Atom Arc 7018 deposition data
- Lincoln Electric, Innershield NR-211-MP data sheet (deposition rates)
- Lincoln Electric, SuperArc L-56 data sheet (melt-off rates)
- Miller Electric, “How to Choose MIG Welding Consumables to Optimize Productivity” (labor share of cost)