To TIG weld 1/8 in mild steel, start at about 95–130 amps on DCEN with a 1/16 in tungsten, a #4–#6 cup, about 11 CFH of argon and 3/32 in ER70S-2 filler rod; 1/8 in aluminum takes about 115–135 amps on AC. Pick your metal, thickness and joint in the TIG welding settings chart below for your own starting amps, tungsten size and type, cup size, argon flow and filler rod, with Miller’s, Lincoln’s and CK Worldwide’s figures side by side.
Your starting TIG settings
Pick the metal, its thickness and the joint. You get a starting amp range, the tungsten, cup, argon flow and filler rod to go with it, and what the other makers’ charts say for the same job.
95–130 A
Miller’s range: 1/8 in mild steel, butt weld
- PolarityDCENTorch on negative (−), clamp on positive (+).
- Tungsten1/16 in2% ceriated (gray) or lanthanated (blue).
- Cup#4–#61/4–3/8 in opening.
- Argon11 CFH5 L/min.
- Filler rod3/32 in ER70S-2
- AC balance75% ENFrequency: Lincoln 90 Hz, Miller 100–180 Hz.
- Lens shadeShade 10–12OSHA minimum 8.
- Watch for
- Starting point. Your machine’s chart wins; run a test bead on scrap.
Show the working
- Amps: Miller’s calculator lists 85–120 A for stainless steel, butt weld.
- Miller lists stainless steel and says to add 10% for mild steel. These amps include it, rounded to 5 A.
- Lincoln Electric: 90–120 A (its 10 gauge, 0.135 in row, any joint). CK Worldwide: 145–205 A, butt or fillet.
- Tungsten size: Miller: 1/16 in (1.6 mm). Lincoln: 3/32 in (2.4 mm).
- 2% ceriated (gray) or 2% lanthanated (blue). Grind it lengthwise to a taper 2–3 times as long as the tungsten is wide, then blunt the very tip.
- Cup: #4–#6 (1/4–3/8 in opening). The number is the opening in sixteenths of an inch.
- Argon, about 11 CFH (5 L/min). Miller’s general advice is 15–20 CFH.
- Filler rod: ER70S-2, 3/32 in (2.4 mm).
- Lens: Shade 10–12 at up to 130 A. OSHA’s minimum is shade 8.
- Figures: Miller’s TIG calculator, Lincoln’s Square Wave TIG 200 guide, CK Worldwide’s technical guide and Hobart’s GTAW guidelines. The full list is at the foot of the page.
TIG welding settings chart
Starting amps by metal, thickness and joint, with the tungsten, cup, argon flow and filler rod for each row. The figures are Miller’s, from its TIG calculator, with Lincoln’s where Miller has no row. The mild steel amps are Miller’s stainless amps plus 10%, as Miller says, rounded to 5 A. Steel and stainless run on DCEN, aluminum on AC. Starred rows have a note under the chart.
| Thickness | Butt weld | Lap weld | Corner weld | Fillet weld | Tungsten | Cup | Gas | Filler rod |
|---|---|---|---|---|---|---|---|---|
| Mild steel (DCEN) | ||||||||
| 24 gauge (0.024 in, 0.6 mm) * | 25–35 A | 25–35 A | 25–35 A | 25–35 A | 1/16 in (1.6 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 7–12 CFH (3–6 L/min) | ER70S-2, 1/16 in (1.6 mm) |
| 1/16 in (1.6 mm, about 16 gauge) | 55–90 A | 65–100 A | 55–90 A | 65–100 A | Miller: 1/16 in (1.6 mm). Lincoln: 3/32 in (2.4 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 11 CFH (5 L/min) | ER70S-2, 1/16 in (1.6 mm) |
| 3/32 in (2.4 mm) | 90–120 A | 100–130 A | 90–120 A | 100–130 A | Miller: 1/16 in (1.6 mm). Lincoln: 3/32 in (2.4 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 11 CFH (5 L/min) | ER70S-2, 1/16 in (1.6 mm) or 3/32 in (2.4 mm) |
| 1/8 in (3.2 mm) | 95–130 A | 110–155 A | 95–130 A | 110–155 A | Miller: 1/16 in (1.6 mm). Lincoln: 3/32 in (2.4 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 11 CFH (5 L/min) | ER70S-2, 3/32 in (2.4 mm) |
| 3/16 in (4.8 mm) * | 140–220 A | 165–220 A | 165–220 A | 195–250 A | 3/32 in (2.4 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 13 CFH (6 L/min) | ER70S-2, 1/8 in (3.2 mm) |
| 1/4 in (6.4 mm) | 250–330 A | 275–360 A | 250–330 A | 275–360 A | 1/8 in (3.2 mm) | #8 (1/2 in opening) | Argon, about 13 CFH (6 L/min) | ER70S-2, 3/16 in (4.8 mm) |
| Stainless steel (DCEN) | ||||||||
| 24 gauge (0.024 in, 0.6 mm) * | 25–35 A | 25–35 A | 25–35 A | 25–35 A | 1/16 in (1.6 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 7–12 CFH (3–6 L/min) | ER308L for 304 stainless, 1/16 in (1.6 mm). ER316L where pitting resistance matters |
| 1/16 in (1.6 mm, about 16 gauge) | 50–80 A | 60–90 A | 50–80 A | 60–90 A | Miller: 1/16 in (1.6 mm). Lincoln: 3/32 in (2.4 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 11 CFH (5 L/min) | ER308L for 304 stainless, 1/16 in (1.6 mm). ER316L where pitting resistance matters |
| 3/32 in (2.4 mm) | 80–110 A | 90–120 A | 80–110 A | 90–120 A | Miller: 1/16 in (1.6 mm). Lincoln: 3/32 in (2.4 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 11 CFH (5 L/min) | ER308L for 304 stainless, 1/16 in (1.6 mm) or 3/32 in (2.4 mm). ER316L where pitting resistance matters |
| 1/8 in (3.2 mm) | 85–120 A | 100–140 A | 85–120 A | 100–140 A | Miller: 1/16 in (1.6 mm). Lincoln: 3/32 in (2.4 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 11 CFH (5 L/min) | ER308L for 304 stainless, 3/32 in (2.4 mm). ER316L where pitting resistance matters |
| 3/16 in (4.8 mm) * | 125–200 A | 150–200 A | 150–200 A | 175–225 A | 3/32 in (2.4 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 13 CFH (6 L/min) | ER308L for 304 stainless, 1/8 in (3.2 mm). ER316L where pitting resistance matters |
| 1/4 in (6.4 mm) | 225–300 A | 250–325 A | 225–300 A | 250–325 A | 1/8 in (3.2 mm) | #8 (1/2 in opening) | Argon, about 13 CFH (6 L/min) | ER308L for 304 stainless, 3/16 in (4.8 mm). ER316L where pitting resistance matters |
| Aluminum (AC) | ||||||||
| 24 gauge (0.024 in, 0.6 mm) * | 25–35 A | 25–35 A | 25–35 A | 25–35 A | 1/16 in (1.6 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 8–15 CFH (4–7 L/min) | ER4043 (general use) or ER5356 (stronger), 1/16 in (1.6 mm) |
| 1/16 in (1.6 mm, about 16 gauge) | 65–75 A | 60–70 A | 55–65 A | 55–75 A | Miller: 1/16 in (1.6 mm). Lincoln: 3/32 in (2.4 mm) | #4–#6 (1/4–3/8 in opening) | Argon, about 15 CFH (7 L/min) | ER4043 (general use) or ER5356 (stronger), 1/16 in (1.6 mm) |
| 3/32 in (2.4 mm) * | 85–110 A | 85–110 A | 85–110 A | 85–110 A | 3/32 in (2.4 mm) | #6–#8 (3/8–1/2 in opening) | Argon, about 10–20 CFH (5–9 L/min) | ER4043 (general use) or ER5356 (stronger), 3/32 in (2.4 mm) |
| 1/8 in (3.2 mm) * | 115–135 A | 105–130 A | 90–120 A | 100–140 A | 3/32 in (2.4 mm) | #6–#7 (3/8–7/16 in opening) | Argon, about 17 CFH (8 L/min) | ER4043 (general use) or ER5356 (stronger), 3/32 in (2.4 mm) |
| 3/16 in (4.8 mm) | 125–150 A | 130–170 A | 130–160 A | 150–180 A | 3/32 in (2.4 mm) | #7–#8 (7/16–1/2 in opening) | Argon, about 21 CFH (10 L/min) | ER4043 (general use) or ER5356 (stronger), 3/32 in (2.4 mm) |
| 1/4 in (6.4 mm) | 190–220 A | 160–180 A | 140–170 A | 170–190 A | 3/32 in (2.4 mm) | #8–#12 (1/2–3/4 in opening) | Argon, about 25 CFH (12 L/min) | ER4043 (general use) or ER5356 (stronger), 3/32 in (2.4 mm) |
- * Mild steel, 24 gauge (0.024 in, 0.6 mm): Lincoln’s range for any joint; Miller’s calculator has no row here. Cup and argon flow are CK Worldwide’s for the tungsten size.
- * Mild steel, 3/16 in (4.8 mm): Miller lists 3/32 in (2.4 mm) or 1/8 in (3.2 mm) tungsten for these joints: lap weld, fillet weld.
- * Stainless steel, 24 gauge (0.024 in, 0.6 mm): Lincoln’s range for any joint; Miller’s calculator has no row here. Cup and argon flow are CK Worldwide’s for the tungsten size.
- * Stainless steel, 3/16 in (4.8 mm): Miller lists 3/32 in (2.4 mm) or 1/8 in (3.2 mm) tungsten for these joints: lap weld, fillet weld.
- * Aluminum, 24 gauge (0.024 in, 0.6 mm): Lincoln’s range for any joint; Miller’s calculator has no row here. Cup and argon flow are CK Worldwide’s for the tungsten size.
- * Aluminum, 3/32 in (2.4 mm): Lincoln’s range for any joint; Miller’s calculator has no row here. Cup and argon flow are CK Worldwide’s for the tungsten size.
- * Aluminum, 1/8 in (3.2 mm): Miller lists 3/32 in (2.4 mm) or 1/8 in (3.2 mm) filler rod for these joints: butt weld.
For aluminum you need an AC/DC TIG welder. Hobart’s guide puts it plainly: a DC machine covers every weldable metal except aluminum and magnesium. Miller adds that inverter welders generally need lower amps than these, and that every figure is approximate.
TIG amperage chart: three makers side by side
The makers do not agree, so here are all three. Miller’s figures are for a butt weld and a fillet weld; Lincoln gives one range for any joint, on a 200 A inverter; CK Worldwide’s tables run hottest. Start low in the spread and work up.
| Thickness | Miller, butt | Miller, fillet | Lincoln, any joint | CK Worldwide, butt | CK Worldwide, fillet |
|---|---|---|---|---|---|
| Mild steel | |||||
| 24 gauge (0.024 in, 0.6 mm) | – | – | 25–35 A | – | – |
| 1/16 in (1.6 mm, about 16 gauge) | 55–90 A | 65–100 A | 70–85 A | 95–135 A | 95–135 A |
| 3/32 in (2.4 mm) | 90–120 A | 100–130 A | 80–100 A | – | – |
| 1/8 in (3.2 mm) | 95–130 A | 110–155 A | 90–120 A | 145–205 A | 145–205 A |
| 3/16 in (4.8 mm) | 140–220 A | 195–250 A | 130–160 A | 210–260 A | 210–260 A |
| 1/4 in (6.4 mm) | 250–330 A | 275–360 A | – | 240–300 A | 240–300 A |
| Stainless steel | |||||
| 24 gauge (0.024 in, 0.6 mm) | – | – | 25–35 A | – | – |
| 1/16 in (1.6 mm, about 16 gauge) | 50–80 A | 60–90 A | 70–85 A | 80–100 A | 90–100 A |
| 3/32 in (2.4 mm) | 80–110 A | 90–120 A | 80–100 A | – | – |
| 1/8 in (3.2 mm) | 85–120 A | 100–140 A | 90–120 A | 120–140 A | 130–150 A |
| 3/16 in (4.8 mm) | 125–200 A | 175–225 A | 130–160 A | 200–250 A | 225–275 A |
| 1/4 in (6.4 mm) | 225–300 A | 250–325 A | – | 275–350 A | 300–375 A |
| Aluminum | |||||
| 24 gauge (0.024 in, 0.6 mm) | – | – | 25–35 A | – | – |
| 1/16 in (1.6 mm, about 16 gauge) | 65–75 A | 55–75 A | 75–85 A | 60–80 A | 70–90 A |
| 3/32 in (2.4 mm) | – | – | 85–110 A | – | – |
| 1/8 in (3.2 mm) | 115–135 A | 100–140 A | 120–135 A | 125–145 A | 140–160 A |
| 3/16 in (4.8 mm) | 125–150 A | 150–180 A | 165–195 A | 195–220 A | 210–240 A |
| 1/4 in (6.4 mm) | 190–220 A | 170–190 A | – | 260–300 A | 280–320 A |
- Lincoln’s steel and stainless rows are 24, 16, 12 and 10 gauge and 3/16 in; its aluminum rows are 24 gauge, 1/16 in, 0.090 in, 1/8 in and 3/16 in. They sit on the nearest row here.
- CK Worldwide’s steel rows are from its low alloy steel table, which covers mild steel. Its 3/16 and 1/4 in aluminum rows use an argon/helium mix.
Print it for the shop
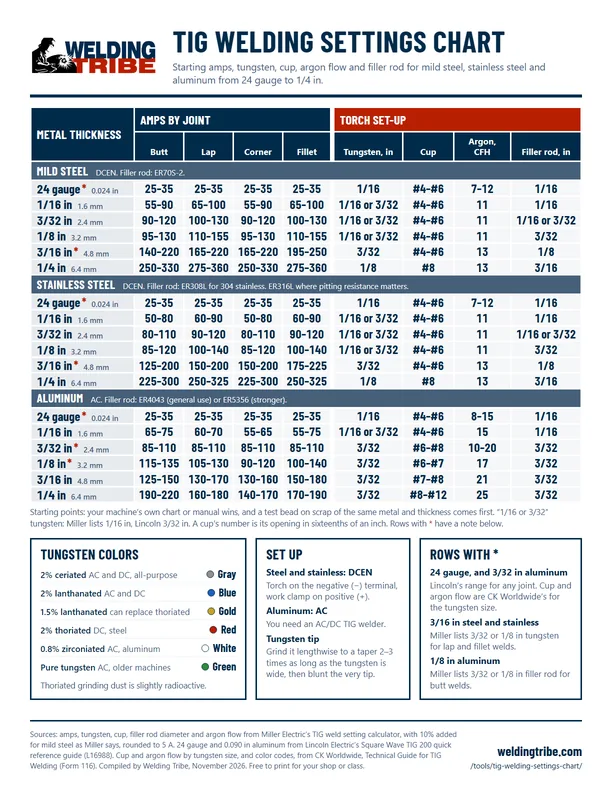
One page, US Letter (it also prints on A4): starting amps by joint for mild steel, stainless steel and aluminum from 24 gauge to 1/4 in, with tungsten, cup, argon flow and filler rod, tungsten colors and the torch hookup. Free, no sign-up.
What size tungsten for TIG welding
Pick the tungsten by the amps it has to carry. The first two columns are from Hobart’s TIG guide, which calls them a composite of American Welding Society recommendations, for 2% ceriated, 1.5% lanthanated or 2% thoriated tungsten in argon. The tip shape matters as well: ground to a point, a tungsten carries less than the same size with a blunt end.
| Tungsten diameter | DCEN (Hobart) | AC, aluminum (Hobart) | AC, balanced wave (CK) | DCEN by tip shape, sharp to blunt (CK, Diamond Ground) | Cup (CK) | Argon, steel (CK) | Argon, aluminum (CK) |
|---|---|---|---|---|---|---|---|
| 0.040 in (1.0 mm) | 15–80 A | 15–80 A | 20–60 A | 2–30 A | #4 or #5 | 5–10 CFH (2–5 L/min) | 5–12 CFH (2–6 L/min) |
| 1/16 in (1.6 mm) | 70–150 A | 70–150 A | 60–120 A | 8–70 A | #4, #5 or #6 | 7–12 CFH (3–6 L/min) | 8–15 CFH (4–7 L/min) |
| 3/32 in (2.4 mm) | 150–250 A | 140–235 A | 100–180 A | 12–150 A | #6, #7 or #8 | 10–15 CFH (5–7 L/min) | 10–20 CFH (5–9 L/min) |
| 1/8 in (3.2 mm) | 250–400 A | 225–325 A | 160–250 A | 20–250 A | #7, #8 or #10 | 10–18 CFH (5–8 L/min) | 12–25 CFH (6–12 L/min) |
- A cup’s number is its opening in sixteenths of an inch: a #6 cup is 3/8 in across and a #8 is 1/2 in. Hobart’s guide asks for an opening at least three times the tungsten’s diameter, and a tungsten that sticks out no farther than that opening.
- CK Worldwide’s argon flows are for a standard collet body; its gas lens figures are lower.
- Tip shape: grind lengthwise, never around the tungsten, on a wheel kept for tungsten only. Hobart’s guide gives a 15–30° point, 30° preferred; CK Worldwide gives a taper 2–3 diameters long with the end blunted. On AC with an old transformer machine, ball the end instead, no wider than the tungsten.
Tungsten color chart
The color band shows what the tungsten is alloyed with. Classes are from AWS A5.12, as CK Worldwide and Diamond Ground list them. Not every maker uses the same colors, so check the box.
| Tungsten | AWS class | Color | Use |
|---|---|---|---|
| 2% ceriated | EWCe-2 | Gray (older stock: orange) | AC and DC. Miller’s all-purpose pick for steel, stainless and aluminum. |
| 2% lanthanated | EWLa-2 | Blue | AC and DC, on Lincoln’s chart. |
| 1.5% lanthanated | EWLa-1.5 | Gold | CK Worldwide lists it as a possible replacement for thoriated. |
| 2% thoriated | EWTh-2 | Red | DC. The traditional pick for steel. Its grinding dust is slightly radioactive. |
| 0.8% zirconiated | EWZr-8 | White | AC. Lincoln calls it a very good choice for aluminum. |
| Pure tungsten | EWP | Green | AC on older transformer machines, with a balled end. Lincoln and Miller advise against it on inverters. |
Red (thoriated) tungsten: its grinding dust carries low-level radioactive material. Hobart’s guide says to think about ceriated or lanthanated instead, and to grind any tungsten with local exhaust or a respirator.
AC balance and frequency for aluminum
These two settings depend on the machine, so treat them as a first try. Miller and Lincoln give balance as the share of each cycle spent electrode negative (EN). More EN gives more penetration and is easier on the tungsten; less EN gives more cleaning. Miller starts a test weld at 75% EN, goes as low as 65% on dirty or old aluminum and no lower than 60%. Lincoln’s Square Wave TIG 200 covers 60–90% EN and 60–150 Hz, with 75% and 90 Hz as its defaults. A higher frequency narrows the arc.
Some machines turn the scale around. Everlast, for one, gives balance as the electrode positive (EP, cleaning) share, and suggests about 20–30% EP. The two always add up to 100%, so 75% EN is 25% EP. Check which one your display shows before you copy a number.
| Joint | Amps | Balance | Frequency |
|---|---|---|---|
| Butt joint | 90–120 A | 65–75% EN | 60–120 Hz |
| T-joint (fillet) | 100–125 A | 70–75% EN | 100–200 Hz |
| Lap joint | 90–110 A | 70–75% EN | 100–150 Hz |
| Corner joint | 80–90 A | 65–70% EN | 100 Hz |
- Hobart’s rows use 1/8 in 5356 filler rod, a 3/32 in 2% ceriated tungsten and argon at 15–20 CFH.
How to hook up a TIG torch
For steel and stainless, TIG runs DCEN: the torch goes on the negative (−) terminal and the work (ground) clamp on positive (+). For aluminum, set the machine to AC. Run the gas hose from the regulator on a cylinder of 100% argon, and plug in the foot pedal or fingertip control.
For which lead goes where on every process, with a diagram, see the welding polarity chart.
Quick answers
How many amps to TIG weld 1/8 inch aluminum?
On AC, Miller’s calculator gives 115–135 A for a butt weld and 100–140 A for a fillet. Lincoln’s chart gives 120–135 A and CK Worldwide’s 125–145 A for a butt weld. Hobart’s guide for inverter machines starts lower, at 90–120 A for a butt joint.
How many amps to TIG weld 1/8 inch steel?
On DCEN, Miller’s figures work out to 95–130 A for a butt weld in mild steel and 110–155 A for a fillet. Stainless needs less: 85–120 A and 100–140 A. Lincoln’s chart gives 90–120 A for 10 gauge steel or stainless, and CK Worldwide’s table runs hotter, at 145–205 A for mild steel.
Is 1 amp per thousandth of an inch right for TIG?
It is a fair first guess, no more. Hobart Brothers gives it as the rule of thumb for aluminum: 1 A per 0.001 in, so about 125 A for 1/8 in and 188 A for 3/16 in. The makers’ charts land on both sides of it. For a butt weld in 1/8 in aluminum: Miller 115–135 A, Lincoln 120–135 A, CK Worldwide 125–145 A. In 3/16 in: Miller 125–150 A, Lincoln 165–195 A, CK Worldwide 195–220 A. Stainless takes less than the rule: Miller lists 85–120 A for a 1/8 in butt weld.
What size tungsten do I need for TIG welding?
Match it to the amps. On DCEN, Hobart’s guide lists 70–150 A for a 1/16 in tungsten, 150–250 A for 3/32 in and 250–400 A for 1/8 in. Miller’s calculator uses 1/16 in up to 1/8 in steel and 3/32 in for most aluminum; Lincoln suggests 3/32 in from 16 gauge up. If you buy one size, Miller calls 3/32 in the general-purpose one.
Do the amps change if I swap a 1/16 tungsten for a 3/32?
No. The amps follow the metal and its thickness. The tungsten only has to carry them: 70–150 A for 1/16 in and 150–250 A for 3/32 in on DCEN, by Hobart’s guide. CK Worldwide’s and Diamond Ground’s tip-shape tables are lower for a ground point: up to 70 A for 1/16 in and up to 150 A for 3/32 in.
Does one tungsten color work for all metals?
Yes. 2% ceriated (gray) and 2% lanthanated (blue) both run on AC and DC, so one box covers steel, stainless and aluminum. Red is 2% thoriated, the traditional DC tungsten. Green is pure tungsten, which Lincoln and Miller advise against on inverter machines.
What cup size for TIG welding?
Miller’s calculator uses a #4–#6 (1/4–3/8 in opening) cup for steel up to 3/16 in, #8 (1/2 in opening) for 1/4 in steel and #6–#7 (3/8–7/16 in opening) for 1/8 in aluminum. For general work, Miller pairs a 3/32 in tungsten with a #8 cup. The number is the opening in sixteenths of an inch.
What should the argon flow rate be for TIG, in CFH?
Miller’s calculator runs from 11 CFH on thin steel to 25 CFH on 1/4 in aluminum (5–12 L/min). Miller’s general advice is 15–20 CFH, and Hobart’s guide gives 10–25 CFH as the typical span. To see how long a cylinder lasts at your flow, use the welding gas cylinder calculator.
Can I use MIG gas for TIG welding?
No. TIG needs an inert gas, and 100% argon covers steel, stainless and aluminum. CK Worldwide warns against the argon/CO2 and argon/oxygen mixes made for MIG.
What filler rod do I use for TIG welding?
Mild steel: ER70S-2, the usual TIG rod (Miller, Hobart Brothers). Stainless: ER308L for 304 (Hobart Brothers lists it for types 201, 302, 304 and 308), or ER316L, which adds molybdenum against pitting. Aluminum: ER4043 for general work, ER5356 for more strength. Miller’s rule for the diameter: no thicker than the metal you are welding. For other stainless grades and stainless to mild steel, see the stainless steel welding rod chart.
A TIG arc is bright even at low amps: pick your lens from the welding shade chart. Running wire instead? The MIG welding settings chart has wire speed and voltage by thickness.
- Amps by joint, tungsten, cup, filler rod diameter and argon flow: Miller Electric’s TIG weld setting calculator, with its notes to add 10% for mild steel and to use a water-cooled torch above 200 A.
- 24 gauge, 0.090 in aluminum and the second set of amps: Lincoln Electric, Square Wave TIG 200 quick reference guide (L16988), which also gives the balance and frequency ranges and its tungsten picks.
- The third set of amps, cup and argon flow by tungsten size, tip shapes and color codes: CK Worldwide, Technical Guide for TIG Welding (Form 116, 2023 update). Diamond Ground Products’ Tungsten Electrode Guidebook has the same tip-shape table and the color codes.
- Tungsten current ranges, grind angle, cup opening, 10–25 CFH, the 1/8 in aluminum joint table and the note on thoriated dust: Hobart Welders, “Guidelines For Gas Tungsten Arc Welding (GTAW)” (215994 F, 2018).
- General settings and AC balance: Miller Electric, “Guide to TIG Welding Basics” (2026) and “How to Implement AC Balance Control for TIG Aluminum Welding” (2025). Balance as percent EP: Everlast.
- Filler rods: Hobart Brothers’ aluminum TIG and solid wire articles and its 308/308L and 316/316L data sheets; Miller Electric, “Choosing What Filler Metal To Use for DIY Welding Projects”.
- Liters per minute are converted from CFH here. Every figure is a starting point for manual welding: your machine’s chart or manual wins, and a test on scrap comes first.
Numbers compiled from the sources below and last updated on . Spotted a mistake? Tell us.
- Miller Electric, TIG weld setting calculator (amps, tungsten, cup, filler rod and argon flow by thickness and joint)
- Lincoln Electric, Square Wave TIG 200 quick reference guide (L16988)
- CK Worldwide, Technical Guide for TIG Welding (Form 116, 2023 update)
- Hobart Welders, “Guidelines For Gas Tungsten Arc Welding (GTAW)” (215994 F, 2018)
- Miller Electric, “Guide to TIG Welding Basics” (2026)
- Miller Electric, “How to Implement AC Balance Control for TIG Aluminum Welding” (2025)
- Miller Electric, “Choosing What Filler Metal To Use for DIY Welding Projects” (2024)
- Diamond Ground Products, “Tungsten Electrode Guidebook” (tip shapes and color codes, after AWS A5.12)
- Hobart Brothers, “5 Tips for Understanding Aluminum TIG Filler Metals, Setup and Welding” (2025)
- Hobart Brothers, “Tips for Choosing a Solid Wire for Welding Applications” (2025)
- Hobart Brothers, 308/308L data sheet (AWS A5.9 ER308, ER308L)
- Hobart Brothers, 316/316L data sheet (AWS A5.9 ER316, ER316L)
- Everlast, “TIG welder setup basics: getting the most out of AC settings” (balance as percent EP)